
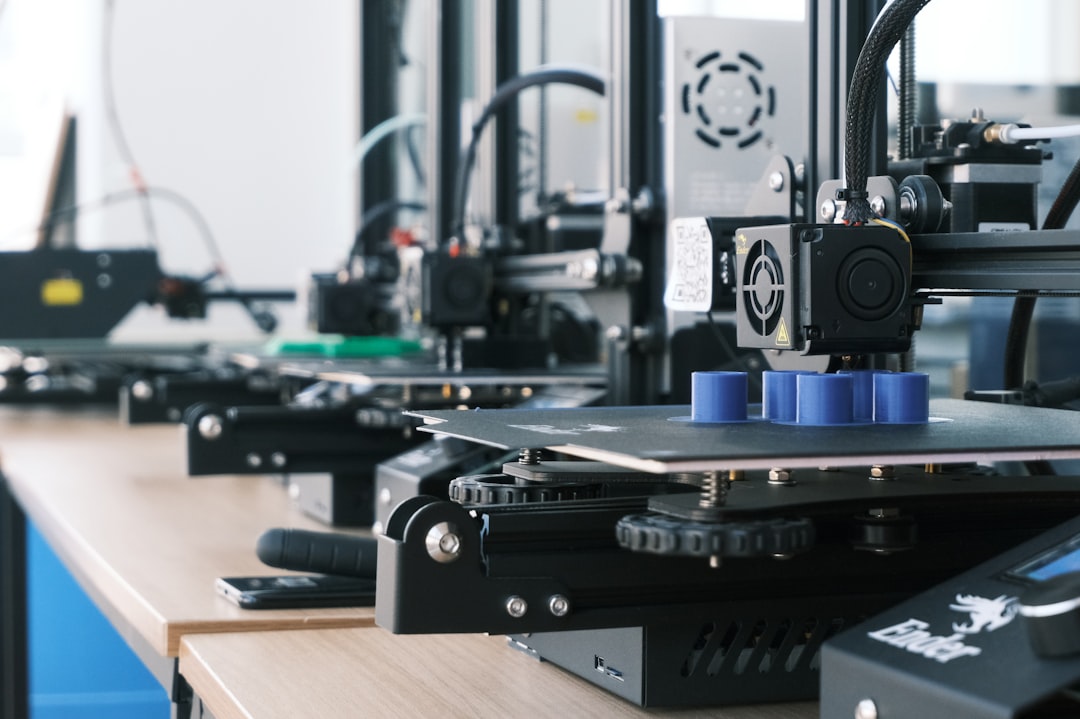
একই STL file একজনের printer-এ সুন্দর result দিল, অন্যজনের machine-এ stringing বা warping হলো—3D printing-এ এটি খুবই সাধারণ। Digital geometry একই থাকলেও manufacturing process-এর অসংখ্য variable final physical object-কে প্রভাবিত করে।

১. Printer আলাদা
Machine-এর frame rigidity, motion system, extruder, hotend, cooling এবং firmware behaviour আলাদা হতে পারে। একই speed setting দুই machine-এ একই acceleration বা vibration তৈরি নাও করতে পারে।
২. Nozzle Diameter
0.4 mm এবং 0.6 mm nozzle একই model-এ line width, detail, wall generation এবং print time বদলে দেয়। Slicer profile nozzle অনুযায়ী না হলে result আরও খারাপ হতে পারে।
৩. Material একই নাম হলেও formulation আলাদা
দুটি brand-এর PLA একই temperature-এ identical flow নাও করতে পারে। PLA+, high-speed PLA বা matte PLA-তে additive আলাদা হতে পারে। Manufacturer recommendation থেকে profile শুরু করা ভালো।

৪. Filament Moisture
এক spool dry, অন্যটি humid environment-এ খোলা থাকলে extrusion quality বদলে যেতে পারে। Bangladesh-এর humidity storage discipline-কে গুরুত্বপূর্ণ করে তোলে।
৫. Slicer Profile
Layer height, wall, flow, speed, acceleration, temperature, retraction এবং cooling—একটি profile-এ বহু setting থাকে। File একই হলেও profile আলাদা হলে toolpath ও physical process আলাদা।
৬. Orientation
একজন model upright, অন্যজন sideways রাখলে support, strength, visible layer এবং print time বদলে যায়। Orientation final result-এর অন্যতম বড় variable।

৭. Build Plate Surface
Smooth PEI, textured plate বা অন্য surface bottom texture এবং adhesion behaviour বদলায়। Plate cleanliness-ও first layer result-এ বড় factor।
৮. Calibration
Z offset, bed leveling, flow calibration, pressure/linear advance বা input shaping machine অনুযায়ী result বদলায়। Modern automatic calibration সাহায্য করলেও mechanical condition ঠিক থাকা দরকার।
৯. Room Environment
Air conditioner-এর draft, open window, enclosure এবং ambient temperature warping-sensitive material-এ বড় পার্থক্য করতে পারে।

১০. Model Revision
Filename একই মনে হলেও file revision আলাদা হতে পারে। Small tolerance change physical fit dramatically বদলাতে পারে। Version naming ও revision control professional project-এ গুরুত্বপূর্ণ।
১১. Support Strategy
Tree/organic support এবং normal support একই underside finish দেয় না। Interface layer, density ও gap result বদলায়।
১২. Print Speed ও Acceleration
High speed-এ hotend যথেষ্ট material melt করতে না পারলে under-extrusion হতে পারে। Motion vibration ringing তৈরি করতে পারে। অন্য printer high-flow hotend ও tuned motion-এর কারণে একই nominal speed ভালোভাবে handle করতে পারে।
১৩. Cooling
Small PLA model-এ strong cooling detail improve করতে পারে, কিন্তু layer bonding-এ trade-off থাকতে পারে। Fan duct design machine অনুযায়ী airflow distribution বদলায়।

১৪. Machine Maintenance
Worn nozzle, loose belt, dirty rod বা damaged build surface print quality degrade করে। একই model কয়েক মাস আগে ভালো print হলেও maintenance issue-এর কারণে পরে খারাপ হতে পারে।
১৫. Operator Decision
3D printing এখনও fully push-button manufacturing নয়। Experienced operator sliced preview দেখে orientation, support এবং profile adjust করতে পারে। Human process knowledge result-এ বড় ভূমিকা রাখে।
Repeatable Result পেতে কী করবেন?
- Printer profile save করুন
- Material brand ও batch note করুন
- Filament dry storage করুন
- Orientation record করুন
- Slicer version ও settings সংরক্ষণ করুন
- Machine maintenance schedule রাখুন
- Critical part-এর dimension log করুন
- Approved revision file আলাদা রাখুন
Production-এর ক্ষেত্রে কেন এটি গুরুত্বপূর্ণ?
একটি client part একবার ভালো print হলেই production-ready নয়। Repeatability দরকার। একই dimension ও appearance multiple unit-এ পাওয়া গেলে process control ভালো বলা যায়। তাই professional 3D printing service-এর value শুধু printer থাকা নয়; repeatable workflow তৈরি করা।
শেষ কথা
একই 3D model different result দেয় কারণ digital file শুধু geometry নির্ধারণ করে; physical manufacturing নির্ধারণ করে machine, material, settings, orientation এবং environment। Artin3D custom ও production project-এ repeatable profile এবং quality-control workflow ব্যবহার করে consistent output পাওয়ার চেষ্টা করে।
Artin3D — আপনার আইডিয়া, আমাদের নিখুঁত বাস্তবতা।


