
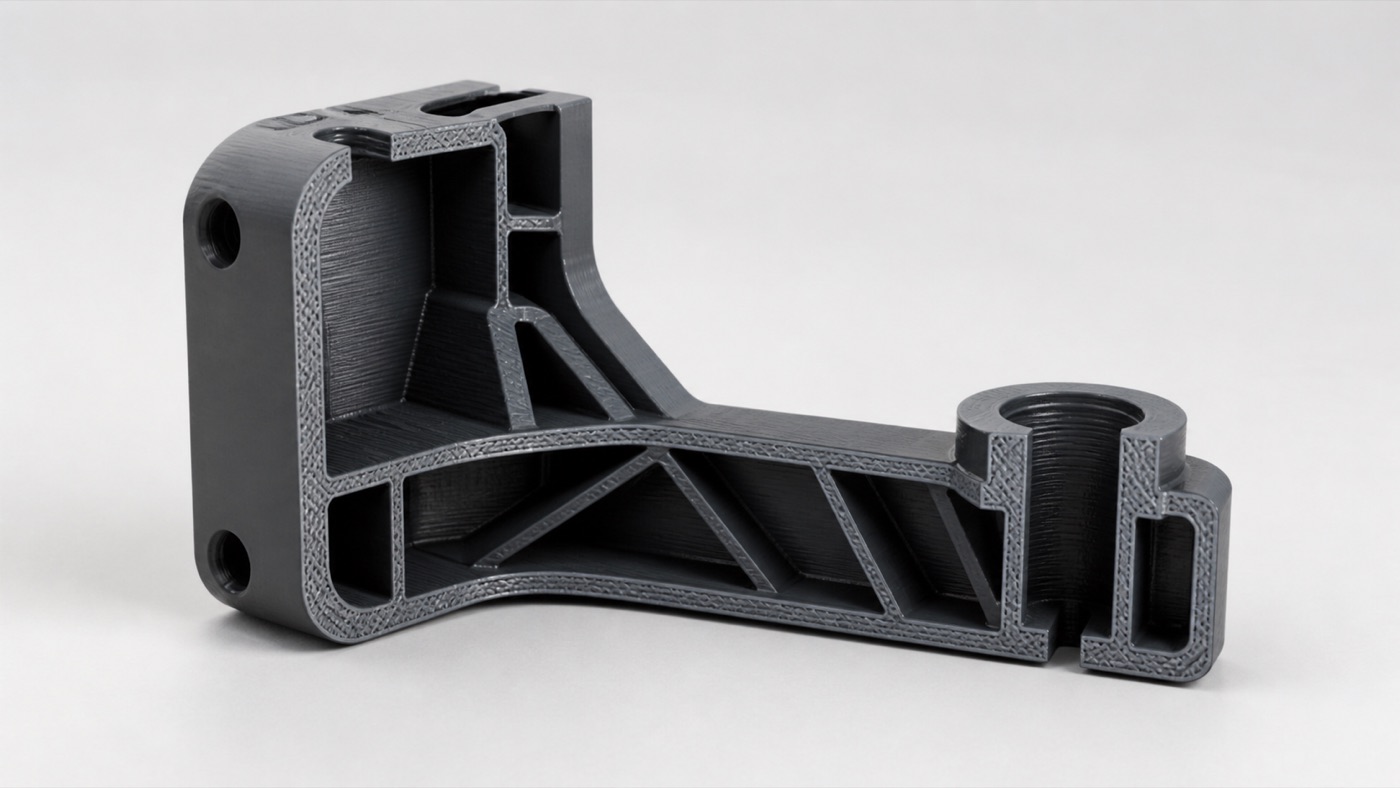
একই 3D model upright, sideways বা tilted করে print করলে final result উল্লেখযোগ্যভাবে বদলে যেতে পারে। Orientation শুধু build plate-এ model বসানোর বিষয় নয়; এটি strength, support, surface finish, dimensional accuracy, print time এবং failure risk-এর ওপর সরাসরি প্রভাব ফেলে।

Orientation কী?
Slicer-এর virtual build plate-এ model কোন angle ও direction-এ রাখা হয়েছে সেটিই orientation। CAD-এ object যেভাবে design করা হয়েছে, সেই direction-এই print করতে হবে এমন কোনো নিয়ম নেই।
১. FDM Strength
FDM part layer-by-layer তৈরি হওয়ায় layer plane এবং layer-to-layer direction-এর mechanical behaviour এক নয়। Load যদি layer আলাদা করার direction-এ পড়ে, failure risk বাড়তে পারে। Functional bracket design-এ expected force direction বুঝে orientation নির্বাচন করা জরুরি।

২. Support Requirement
একটি model vertical রাখলে বড় overhang হতে পারে, কিন্তু 90 degree rotate করলে support কমে যেতে পারে। আবার support কমানোর জন্য rotate করলে strength বা visible surface খারাপ হতে পারে। তাই একাধিক factor balance করতে হয়।
৩. Surface Finish
Support contact surface সাধারণত clean free surface-এর মতো হয় না। Presentation model-এ important visible face support থেকে দূরে রাখা ভালো। Curved surface-এর staircase effect-ও orientation অনুযায়ী বদলায়।
৪. Print Time
FDM-এ object-এর Z height বাড়লে layer count বাড়ে। Tall orientation অনেক ক্ষেত্রে বেশি সময় নিতে পারে। তবে footprint, travel এবং support-ও total time-এ ভূমিকা রাখে। Slicer estimate compare করা useful।

৫. Build Plate Adhesion
Very small contact area-তে tall part print করলে wobble বা detachment risk বাড়তে পারে। Larger stable footprint adhesion improve করতে পারে। Brim ব্যবহার করা গেলেও orientation fundamentally unstable হলে redesign ভালো solution হতে পারে।
৬. Dimensional Accuracy
Vertical hole এবং horizontal hole একইভাবে print হয় না। Circular feature layer stepping ও extrusion behaviour-এর কারণে axis অনুযায়ী different accuracy পেতে পারে। Critical bearing বা shaft fit-এ orientation test গুরুত্বপূর্ণ।
৭. Seam Location
FDM perimeter start/stop point visible seam তৈরি করতে পারে। Orientation ও seam placement strategy cosmetic surface-এর appearance বদলায়।

৮. Text এবং Logo
Embossed বা engraved text কোন plane-এ আছে তার ওপর readability নির্ভর করতে পারে। Very small vertical text এবং top-facing text-এর result আলাদা হতে পারে।
৯. Split Part Assembly
Large model split করলে প্রতিটি section এমন orientation-এ print করা যায় যাতে visible face clean থাকে। Joint line hidden location-এ রাখলে finishing সহজ হয়।
Resin Printing-এ Orientation কেন আরও গুরুত্বপূর্ণ?
Resin process-এ প্রতিটি cured layer release film থেকে separate হয়। Large cross-sectional area peel force বাড়াতে পারে। Model tilt করলে cross-section reduce, support placement improve এবং suction-related issue কমানো যেতে পারে। Hollow model-এ drainage orientation-ও গুরুত্বপূর্ণ।

Orientation বাছাইয়ের Practical Method
- Part-এর primary function নির্ধারণ করুন
- Expected load direction চিহ্নিত করুন
- Important cosmetic face mark করুন
- Critical dimension/holes চিহ্নিত করুন
- Different orientation-এ support compare করুন
- Slicer time ও material estimate compare করুন
- Risky tall/narrow geometry check করুন
- Prototype test করুন
শুধু Auto Orient-এর ওপর নির্ভর করবেন?
Auto orientation useful starting point হতে পারে, কিন্তু software আপনার product-এর real-world load, visible face বা assembly priority সবসময় জানে না। Final decision human design intent অনুযায়ী review করা উচিত।
শেষ কথা
Orientation হলো zero-cost design decision যা material পরিবর্তন না করেই একটি print-এর strength, finish এবং success rate বদলে দিতে পারে। Professional workflow-এ Print চাপার আগে orientation review অত্যন্ত গুরুত্বপূর্ণ। Artin3D প্রতিটি custom part-এর application অনুযায়ী orientation ও support strategy নির্বাচন করে।
Artin3D — আপনার আইডিয়া, আমাদের নিখুঁত বাস্তবতা।


