Display model সুন্দর দেখালেই যথেষ্ট নয়—size, viewing distance, transport, paint, deadline ও budget ঠিক করে FDM, SLA নাকি hybrid process সবচেয়ে যুক্তিযুক্ত।
একটি 300 mm architectural massing model এবং 32 mm character miniature দুটোই display model, কিন্তু production need বিপরীত। বড় simple form FDM-এ দ্রুত ও economical; ছোট facial detail SLA-তে পরিষ্কার। Technology brand নিয়ে debate না করে model requirement ভাগ করলে সিদ্ধান্ত সহজ হয়।
অনেক project-এ hybrid answer সেরা: বড় base ও structure FDM, small ornament ও hero detail SLA। Assembly, colour ও finishing পরিকল্পনা করলে দুই process-এর শক্তি ব্যবহার করে cost নিয়ন্ত্রণে রাখা যায়।
সংক্ষিপ্ত উত্তর
বড়, কম-detail, durable ও budget-sensitive display-এর জন্য FDM; ছোট, high-detail, smooth ও close-viewed model-এর জন্য SLA। বড় model-এ শুধু কয়েকটি hero detail থাকলে FDM body + SLA detail hybrid workflow প্রায়ই সর্বোত্তম।
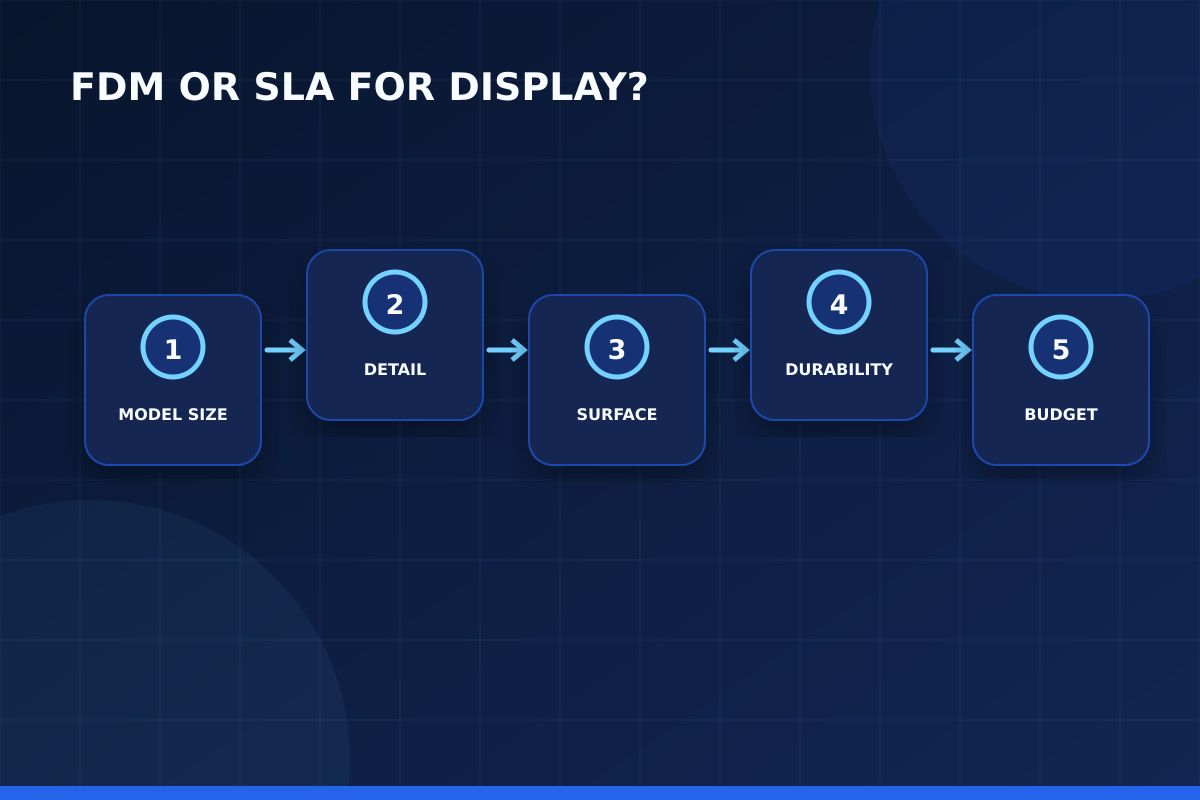
Model Size ও Build Volume
FDM printer সাধারণত তুলনামূলক বড় build volume এবং কম material cost দেয়। Large prop, architectural volume, product mock-up ও statue shell-এ এটি সুবিধাজনক। SLA build area ছোট এবং resin weight/cost দ্রুত বাড়ে। বড় resin shell hollow করলেও drain, support ও wash complexity থাকে। Final model split ও seam কোথায় হবে আগে পরিকল্পনা করুন।
একটি নির্ভরযোগ্য workflow হলো একবারে একটি variable পরিবর্তন করা। প্রথম test-এর ছবি, resin batch, temperature, layer height ও exposure লিখে রাখুন। পরের test-এ শুধু একটি parameter বদলান। এতে improvement কোন পরিবর্তনের কারণে হয়েছে বোঝা যায়; একই সঙ্গে ভবিষ্যতের repeat order-এ consistent result পাওয়া সহজ হয়।
Detail ও Viewing Distance
Model 2–3 meter দূর থেকে দেখা হলে 0.1 mm micro texture প্রয়োজন নাও হতে পারে। Trade-show prop-এ silhouette ও colour বেশি গুরুত্বপূর্ণ। কিন্তু handheld miniature বা product hero model কাছ থেকে দেখা হয়, সেখানে SLA facial feature, tiny logo ও smooth curve ভালো ধরে। Required detail viewing distance থেকে reverse-engineer করুন।
ছোট feature-এর ক্ষেত্রে digital model-এর detail থাকাই যথেষ্ট নয়; printer-এর XY resolution, layer height, resin behavior এবং cleaning method সেই detail বাঁচাতে পারছে কি না সেটিও জরুরি। Design-এর সবচেয়ে পাতলা অংশ printer-এর practical limit-এর কাছাকাছি হলে সামান্য scale increase বা controlled thickening অনেক সময় দৃশ্যমান পার্থক্য তৈরি করে।
Surface Finish ও Layer Lines
FDM-এ curved surface-এ visible layer line থাকে, বিশেষ করে বড় layer height-এ। Sanding, filler primer ও paint দিয়ে smooth করা যায়, কিন্তু labour যোগ হয়। SLA raw surface smooth হলেও support side finish করতে হয় এবং cure/primer লাগে। Quotation-এ print price নয়, finished appearance পর্যন্ত total labour compare করুন।
Safety-কে finishing-এর আলাদা বিষয় ভাবা ঠিক নয়। Uncured resin skin contact এড়াতে উপযুক্ত nitrile glove, eye protection ও পরিষ্কার work area দরকার। Resin এবং contaminated cleaning liquid স্থানীয় নিয়ম মেনে dispose করতে হবে; sink বা খোলা জায়গায় ফেলা উচিত নয়। নির্দিষ্ট wash ও cure time সবসময় resin manufacturer-এর নির্দেশনা অনুযায়ী ঠিক করুন।
Strength, Handling ও Transport
Large display বারবার setup, courier বা exhibition handling পেলে FDM thermoplastic shell অনেক ক্ষেত্রে বেশি forgiving। Standard resin thin protrusion drop-এ ভাঙতে পারে। Tough resin সাহায্য করে কিন্তু cost বাড়ায়। Detachable peg, magnet, internal rod ও transport case technology choice-এর পাশাপাশি durability বাড়াতে পারে।
Professional result-এর জন্য “আরও বেশি” সবসময় “আরও ভালো” নয়। বেশি exposure fine gap বন্ধ করতে পারে, বেশি support surface নষ্ট করতে পারে, বেশি cure brittleness বাড়াতে পারে এবং aggressive washing সূক্ষ্ম অংশ ভেঙে দিতে পারে। লক্ষ্য হলো model ও resin অনুযায়ী balanced setting, সর্বোচ্চ setting নয়।
Colour ও Multi-part Assembly
FDM multi-colour filament বা আলাদা coloured part দিয়ে presentation-ready result দিতে পারে; SLA সাধারণত paint workflow-এ শক্তিশালী। Fine resin pieces paint করে FDM body-তে assemble করা যায়। Seam, locating pin, adhesive gap ও paint tolerance CAD-এ রাখুন। Transparent component-এর optical clarity raw resin দিয়ে automatic নয়; polishing ও coating লাগতে পারে।
Batch production-এর আগে একটি approved master sample রাখা কার্যকর। সেই sample-এর dimensions, surface, support marks ও colour দেখে পরবর্তী batch তুলনা করা যায়। একই model আবার print করতে হলে resin ভালোভাবে mix করা, tank inspect করা এবং validated file ব্যবহার করা consistency বাড়ায়।
Print Time ও Deadline
FDM time toolpath length ও layer heightে বাড়ে; একই plate-এ object বাড়লে সময়ও বাড়ে। Resin printer একটি layer একসঙ্গে expose করায় এক height-এর অনেক ছোট model efficient হতে পারে, তবে Z height এবং post-processing time থাকে। Deadline হিসাবের সময় failed print allowance, cooling/draining, wash, cure, sanding ও paint অন্তর্ভুক্ত করুন।
Cost হিসাবেও failed print-এর প্রভাব বড়। শুধু model-এর resin নয়, support, wash liquid, gloves, machine time এবং finishing labour যোগ হয়। তাই preparation-এ কয়েক মিনিট বেশি ব্যয় করে orientation ও support review করা প্রায়ই দ্রুত print শুরু করার চেয়ে লাভজনক।
Cost per Finished Model
FDM filament সাধারণত কম খরচের এবং support waste কমানো সহজ। SLA resin, support, solvent, glove ও cure labour যোগ করে। কিন্তু FDM smooth করতে বহু ঘণ্টা sanding লাগলে total cost উল্টো বাড়তে পারে। Cost model-এ machine hour, material, failure risk এবং finishing hour আলাদা line item রাখুন।
Resin printing-এ কোনো setting আলাদাভাবে কাজ করে না। Layer height, exposure, lift movement, support এবং model geometry একে অন্যকে প্রভাবিত করে। তাই production model-এ যাওয়ার আগে একই resin, একই room condition এবং একই profile দিয়ে ছোট validation print করা ভালো। এতে failure হলে কারণ চিহ্নিত করা সহজ হয় এবং অপ্রয়োজনীয় resin নষ্ট কমে।
Hybrid Technology কখন সেরা
Architectural model-এর terrain/base FDM এবং facade ornament SLA; character statue-এর torso FDM এবং face/accessory SLA; product mock-up-এর housing FDM এবং button/logo insert SLA—এভাবে hybrid ব্যবহার করা যায়। CAD split line hidden seam-এ রাখুন, alignment pin দিন এবং material-specific adhesive test করুন। Final primer দুই material-এর colour unify করতে পারে।
প্র্যাকটিক্যাল সিদ্ধান্ত নেওয়ার সময় শুধু screen preview দেখে থেমে গেলে চলবে না। Model-এর visible face, load direction, trapped resin, suction force এবং পরে support removal—সবগুলো ধাপ একসঙ্গে কল্পনা করতে হবে। যে orientation print সফল করে কিন্তু গুরুত্বপূর্ণ face-এ গভীর mark রেখে দেয়, সেটিকে ভালো orientation বলা যায় না।
ধাপে ধাপে Practical Workflow
- Final size ও viewing distance লিখুন।
- Hero detail ও simple volume আলাদা করুন।
- Handling, transport ও heat exposure নির্ধারণ করুন।
- FDM, SLA ও hybrid-এর finished-cost compare করুন।
- Representative surface sample print করুন।
- Split, pin, magnet ও seam CAD-এ design করুন।
- Paint/primer compatibility test করুন।
- Approved master অনুযায়ী batch plan করুন।
দ্রুত সিদ্ধান্তের Checklist
- Model হাতে ধরে দেখা হবে?
- Size printer build volume-এর মধ্যে?
- Thin fragile detail আছে?
- Sanding/painting budget আছে?
- Transport কতবার হবে?
- Hybrid split seam লুকানো যায়?
Common Mistakes
- Raw print price দিয়েই decision নেওয়া।
- সব বড় model SLA-তে করে cost বাড়ানো।
- সব ছোট detail FDM-এ রেখে finishing labour বাড়ানো।
- Transport strength না ভাবা।
- Hybrid part-এর tolerance না রাখা।
প্রায় জিজ্ঞাসিত প্রশ্ন
Figurine-এর জন্য FDM ব্যবহার করা যায়?
বড় stylized figure-এ যায়। 28–75 mm high-detail face ও texture-এর জন্য SLA সাধারণত cleaner result দেয়।
Architectural model কোন process-এ ভালো?
Massing, base ও বড় building FDM; facade ornament, furniture ও tiny figure SLA—hybrid approach কার্যকর।
SLA কি সবসময় smooth?
Top/side surface smooth হতে পারে, কিন্তু support side mark ও staircase থাকে। Correct orientation ও finishing এখনও দরকার।
FDM smooth করতে কী লাগে?
Lower layer, good orientation, sanding, filler primer ও paint ব্যবহার করা যায়। Geometry ও material অনুযায়ী method বাছাই করুন।
কোনটি দ্রুত?
Model-dependent। বড় simple part FDM economical; একই height-এর বহু tiny part resin plate-এ efficient হতে পারে। Post-processingসহ total lead time compare করুন।
Hybrid model-এর joint দেখা যাবে?
ভালো split line, pin, gap control, filler ও uniform primer ব্যবহার করলে seam অনেক কমানো যায়।
বাস্তব প্রয়োগের নোট 1: Model Size ও Build Volume
FDM printer সাধারণত তুলনামূলক বড় build volume এবং কম material cost দেয়। Large prop, architectural volume, product mock-up ও statue shell-এ এটি সুবিধাজনক। SLA build area ছোট এবং resin weight/cost দ্রুত বাড়ে। বড় resin shell hollow করলেও drain, support ও wash complexity থাকে। Final model split ও seam কোথায় হবে আগে পরিকল্পনা করুন। Professional result-এর জন্য “আরও বেশি” সবসময় “আরও ভালো” নয়। বেশি exposure fine gap বন্ধ করতে পারে, বেশি support surface নষ্ট করতে পারে, বেশি cure brittleness বাড়াতে পারে এবং aggressive washing সূক্ষ্ম অংশ ভেঙে দিতে পারে। লক্ষ্য হলো model ও resin অনুযায়ী balanced setting, সর্বোচ্চ setting নয়। এই পর্যবেক্ষণটি FDM vs SLA Display Model নিয়ে কাজ করার সময় decision log-এ লিখে রাখলে পরবর্তী print বা production batch-এ একই ভুল পুনরাবৃত্তি হওয়ার ঝুঁকি কমে।
বাস্তব প্রয়োগের নোট 2: Detail ও Viewing Distance
Model 2–3 meter দূর থেকে দেখা হলে 0.1 mm micro texture প্রয়োজন নাও হতে পারে। Trade-show prop-এ silhouette ও colour বেশি গুরুত্বপূর্ণ। কিন্তু handheld miniature বা product hero model কাছ থেকে দেখা হয়, সেখানে SLA facial feature, tiny logo ও smooth curve ভালো ধরে। Required detail viewing distance থেকে reverse-engineer করুন। Batch production-এর আগে একটি approved master sample রাখা কার্যকর। সেই sample-এর dimensions, surface, support marks ও colour দেখে পরবর্তী batch তুলনা করা যায়। একই model আবার print করতে হলে resin ভালোভাবে mix করা, tank inspect করা এবং validated file ব্যবহার করা consistency বাড়ায়। এই পর্যবেক্ষণটি FDM vs SLA Display Model নিয়ে কাজ করার সময় decision log-এ লিখে রাখলে পরবর্তী print বা production batch-এ একই ভুল পুনরাবৃত্তি হওয়ার ঝুঁকি কমে।
বাস্তব প্রয়োগের নোট 3: Surface Finish ও Layer Lines
FDM-এ curved surface-এ visible layer line থাকে, বিশেষ করে বড় layer height-এ। Sanding, filler primer ও paint দিয়ে smooth করা যায়, কিন্তু labour যোগ হয়। SLA raw surface smooth হলেও support side finish করতে হয় এবং cure/primer লাগে। Quotation-এ print price নয়, finished appearance পর্যন্ত total labour compare করুন। Cost হিসাবেও failed print-এর প্রভাব বড়। শুধু model-এর resin নয়, support, wash liquid, gloves, machine time এবং finishing labour যোগ হয়। তাই preparation-এ কয়েক মিনিট বেশি ব্যয় করে orientation ও support review করা প্রায়ই দ্রুত print শুরু করার চেয়ে লাভজনক। এই পর্যবেক্ষণটি FDM vs SLA Display Model নিয়ে কাজ করার সময় decision log-এ লিখে রাখলে পরবর্তী print বা production batch-এ একই ভুল পুনরাবৃত্তি হওয়ার ঝুঁকি কমে।
বাস্তব প্রয়োগের নোট 4: Strength, Handling ও Transport
Large display বারবার setup, courier বা exhibition handling পেলে FDM thermoplastic shell অনেক ক্ষেত্রে বেশি forgiving। Standard resin thin protrusion drop-এ ভাঙতে পারে। Tough resin সাহায্য করে কিন্তু cost বাড়ায়। Detachable peg, magnet, internal rod ও transport case technology choice-এর পাশাপাশি durability বাড়াতে পারে। Resin printing-এ কোনো setting আলাদাভাবে কাজ করে না। Layer height, exposure, lift movement, support এবং model geometry একে অন্যকে প্রভাবিত করে। তাই production model-এ যাওয়ার আগে একই resin, একই room condition এবং একই profile দিয়ে ছোট validation print করা ভালো। এতে failure হলে কারণ চিহ্নিত করা সহজ হয় এবং অপ্রয়োজনীয় resin নষ্ট কমে। এই পর্যবেক্ষণটি FDM vs SLA Display Model নিয়ে কাজ করার সময় decision log-এ লিখে রাখলে পরবর্তী print বা production batch-এ একই ভুল পুনরাবৃত্তি হওয়ার ঝুঁকি কমে।
বাস্তব প্রয়োগের নোট 5: Colour ও Multi-part Assembly
FDM multi-colour filament বা আলাদা coloured part দিয়ে presentation-ready result দিতে পারে; SLA সাধারণত paint workflow-এ শক্তিশালী। Fine resin pieces paint করে FDM body-তে assemble করা যায়। Seam, locating pin, adhesive gap ও paint tolerance CAD-এ রাখুন। Transparent component-এর optical clarity raw resin দিয়ে automatic নয়; polishing ও coating লাগতে পারে। প্র্যাকটিক্যাল সিদ্ধান্ত নেওয়ার সময় শুধু screen preview দেখে থেমে গেলে চলবে না। Model-এর visible face, load direction, trapped resin, suction force এবং পরে support removal—সবগুলো ধাপ একসঙ্গে কল্পনা করতে হবে। যে orientation print সফল করে কিন্তু গুরুত্বপূর্ণ face-এ গভীর mark রেখে দেয়, সেটিকে ভালো orientation বলা যায় না। এই পর্যবেক্ষণটি FDM vs SLA Display Model নিয়ে কাজ করার সময় decision log-এ লিখে রাখলে পরবর্তী print বা production batch-এ একই ভুল পুনরাবৃত্তি হওয়ার ঝুঁকি কমে।
বাস্তব প্রয়োগের নোট 6: Print Time ও Deadline
FDM time toolpath length ও layer heightে বাড়ে; একই plate-এ object বাড়লে সময়ও বাড়ে। Resin printer একটি layer একসঙ্গে expose করায় এক height-এর অনেক ছোট model efficient হতে পারে, তবে Z height এবং post-processing time থাকে। Deadline হিসাবের সময় failed print allowance, cooling/draining, wash, cure, sanding ও paint অন্তর্ভুক্ত করুন। একটি নির্ভরযোগ্য workflow হলো একবারে একটি variable পরিবর্তন করা। প্রথম test-এর ছবি, resin batch, temperature, layer height ও exposure লিখে রাখুন। পরের test-এ শুধু একটি parameter বদলান। এতে improvement কোন পরিবর্তনের কারণে হয়েছে বোঝা যায়; একই সঙ্গে ভবিষ্যতের repeat order-এ consistent result পাওয়া সহজ হয়। এই পর্যবেক্ষণটি FDM vs SLA Display Model নিয়ে কাজ করার সময় decision log-এ লিখে রাখলে পরবর্তী print বা production batch-এ একই ভুল পুনরাবৃত্তি হওয়ার ঝুঁকি কমে।
শেষ কথা
Display model-এর technology selection binary নয়। Scale, detail, viewing distance, handling এবং finished-cost মিলিয়ে FDM, SLA বা hybrid বেছে নিতে হয়।
Client presentation-এর আগে একটি surface/colour sample approve করলে final model নিয়ে expectation পরিষ্কার থাকে এবং rework কমে।
আপনার model, sample, measurement বা project requirement পাঠালে Artin3D team printability, material, orientation এবং finishing requirement review করে উপযুক্ত solution প্রস্তাব করতে পারে। Artin3D-এর সঙ্গে যোগাযোগ করুন।
Artin3D – Where ideas take shape.